
Get in Touch with Saiweiglass


Optical Bonding Solutions — Professional Glass-to-Display Bonding Services
We eliminate the air gap between your cover glass and lcd panel to deliver optically bonded displays with superior sunlight readability, condensation prevention, and impact resistance. From prototype to mass production.
10+
Years Experience
1M+
Annual Capacity
3
Factories
50+
Technicians
What Is Optical Bonding?
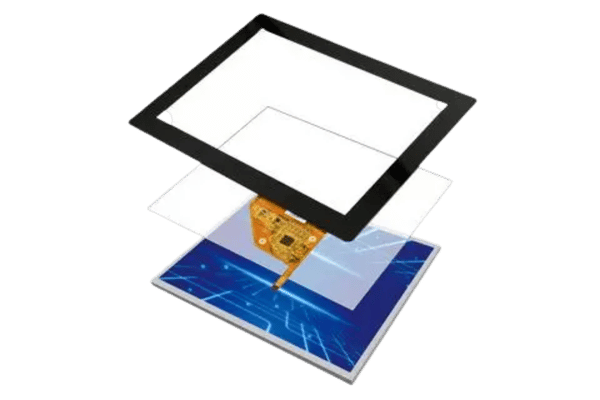
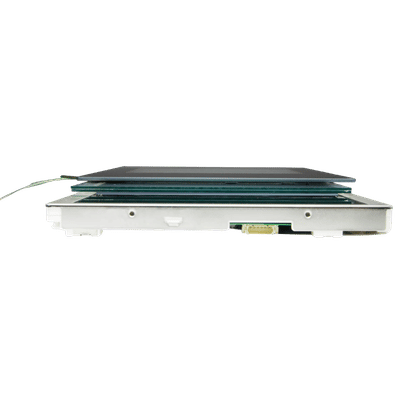
Optical bonding is a manufacturing process that permanently attaches a protective glass or touchscreen panel to an LCD display using an optically clear adhesive. The goal: eliminate the air gap that causes glare, condensation, and reduced readability in harsh environments.
In a standard display assembly, the cover glass sits above the lcd panel with a thin layer of air between them. That air gap creates two additional glass-to-air interfaces where light undergoes refraction and internal reflection. The result is washed-out images, especially under direct sunlight, and a space where dust and moisture can accumulate over time.
An optically bonded display replaces that air gap with a layer of adhesive whose refractive index closely matches glass (typically 1.47-1.50). This dramatically reduces reflections at the bonding interfaces and creates a monolithic optical stack. The practical outcome: improved contrast ratio, accurate touch response on touchscreen panels, and a sealed assembly that resists condensation, vibration, and impact.
How Optical Bonding Works — The Process
The optical bonding process varies based on whether LOCA or OCA adhesive is used, but the core sequence follows the same logic:
01
Surface Cleaning & Plasma Treatment
02
Adhesive Application (LOCA Dispense or OCA Lamination)
03
Vacuum Defoaming & Alignment
04
UV Light Cure or Pressure Cure
05
QC Inspection & Bond Strength Test
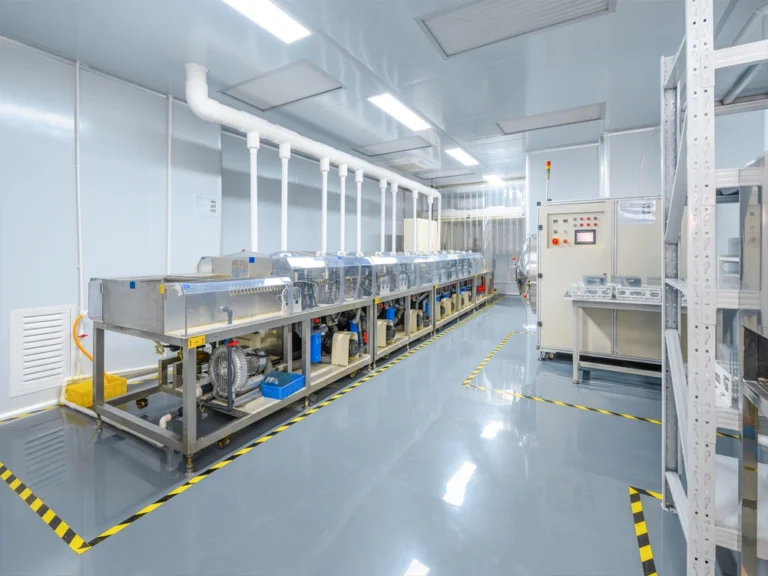
Cleaning is critical. Even a single particle trapped in the bond line creates a visible defect. Our 10-tank ultrasonic cleaning line removes sub-micron contaminants before plasma treatment activates the glass surface for optimal adhesive wetting. After adhesive application, vacuum defoaming removes trapped air bubbles-a step that separates reliable optical bonding from poor-quality assemblies that develop voids over time.
Optical Bonding vs Air Bonding — Key Differences
Air bonding (also called air-gap bonding) simply holds the cover glass above the display using a gasket or frame, leaving the air gap intact. Here is how the two approaches compare with real-world performance data:
| Parameter | Optical Bonding | Air Bonding (Air Gap) |
|---|---|---|
| Air Gap | Eliminated | Present (0.3–1.0 mm typical) |
| Surface Reflection | ~0.5–1.5% | ~4–8% |
| Sunlight Readability | Excellent—high contrast ratio maintained | Poor under direct sunlight |
| Condensation Risk | None—sealed bond | High in humid/marine environments |
| Impact / Shock Resistance | High—adhesive absorbs energy | Depends on glass support, mounting and assembly design |
| Touch Accuracy | Improved—reduced parallax | Standard |
| Display Brightness Needed | Lower (saves power) | Higher backlight required |
| Weight | Slightly higher (+adhesive layer) | Slightly lighter |
| Reworkability | Limited (LOCA) / Moderate (OCA) | Easy disassembly |
| Cost | Higher per unit | Lower per unit |
Our take:
Air bonding makes sense for indoor, climate-controlled applications where cost is the primary driver. But for any display facing sunlight, temperature swings, vibration, or moisture-industrial HMIs, marine electronics, medical devices, automotive dashboards-optical bonding pays for itself through reduced field failures and improved operator usability. We have seen customers switch from air bonding to optical bonding after experiencing condensation failures in the field, and the total cost of rework always exceeds the upfront bonding investment.
Types of Optical Bonding Materials — LOCA, OCA & More
The adhesive is the heart of any optical bonding process. Choosing the right material determines optical performance, durability, temperature range, and reworkability of the bonded display assembly.
LOCA Bonding (Liquid Optically Clear Adhesive)
LOCA is a liquid resin-typically silicone-based, polyurethane, or epoxy-based-dispensed directly onto the display surface. After the cover glass is aligned and placed, uv light initiates the cure cycle that converts the liquid adhesive into a solid, transparent bond layer.
When we recommend LOCA: Non-standard panel sizes, curved displays, assemblies with uneven surfaces or large gaps, and applications requiring wide temperature tolerance (-40 C to +85 C). LOCA excels where the adhesive needs to flow and conform. Its main trade-off: the bonding process is slower and more operator-dependent, and rework is difficult once cured.
ASK how adhesive volume, dispensing pattern and bubble control process will be established for your panel geometry. AGREE on clearances from display edges and connectors and limits for voids and adhesive overflow.
OCA Bonding (Optically Clear Adhesive)
Film OCA is an optically clear adhesive supplied as a film and laminated between compatible display layers. Processing depends on the product: pressure-sensitive grades and grades requiring UV curing after lamination are both available.
When do we specify OCA: standard rectangular panels, high throughput, time-critical production runs, applications where future rework of the display structure may be anticipated. OCA films tend to have incredibly evenly bond-line thickness (50 – 200 m typical), which is important to optical uniformity across the display.
The problem: OCA films are not flexible to uneven topographies, deep step heights or curved geometries. For panel pcs and flat cover glass industrial touchscreen, the use of OCA tends to be the better approach in most cases.
Choosing the Right Adhesive for Your Application
| Criteria | LOCA | OCA |
|---|---|---|
| Surface Conformity | Excellent | Good (flat surfaces) |
| Bond Uniformity | Operator-dependent | Factory-controlled thickness |
| Cure Method | UV light / thermal | Pressure (no cure needed) |
| Cycle Time | Longer (cure step) | Shorter |
| Reworkability | Difficult | Moderate (heat separation) |
| Curved / Irregular Shapes | Yes | Limited |
| Temperature Range | -40 to +85 °C typical | -30 to +80 °C typical |
| Best For | Marine, aerospace, large/custom panels | Panel PCs, standard HMIs, high-volume |
What we sometimes do in practice:
Use a hybrid structure. If Anlinis lcd panel with a deeper bezel step, using OCA in the active display area and a LoCA fill for the step between the bezel and the glass edge can work fine. The optimum solution depends on the geometry, volume, and environmental sensitivity.
Not sure which adhesive is right for your project?
Discuss Your Requirements with Our EngineersBenefits of Optical Bonding for Industrial Displays
Optical bonding provides measurable benefits in four key areas. These are not just theoretical advantages-they are the basis for the choice for customers in the marine, medical, industrial sectors who specify optically bonded displays.
Enhanced Sunlight Readability & Reduced Glare
Any light incident on a glass-to-air interface is reflected. In a typical air-bonded assembly, there are four glass-to-air interfaces, which produce up to 8% reflection. The second optical bonding eliminates the air gap interface reduces this to about 1.5%. The display can be easily read in direct sunlight without maximum backlighting, which is both power-efficient and system-efficient.
Improved Durability & Shock Resistance
Improving display ruggedness with optical-bonding materials relies on adhesive and assembly design. Define the required impact, shock and vibration tests. Request the complete test assembly results. Do not assume that bonding makes glass unbreakable or that bonding establishes fragment retention.
Accurate Touch Response & Sensitivity
Reducing visual parallax between the touch surface and displayed image with optical bonding does not establish an improvement in touch-sensor accuracy. Confirm touch performance of the complete assembly under the required operating conditions.
Condensation Prevention & Environmental Protection
Filling the gap between the display and cover removes a space where internal condensation may form. Confirm moisture protection, humidity and temperature-cycling performance for the complete assembly. Request enclosure-level evidence for any specified IP rating.
Optical Bonding Applications by Industry
Optically bonded glass assemblies we produce for five large sectors, each with different glass type, surface treatment, environmental sealants, and certification.
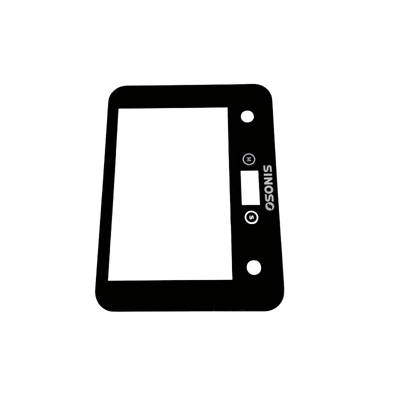
Industrial Touch Panels & HMI Displays
When specifying factory automation systems (i.e. Panel PCs, CNC controls and SCADA interfaces), define the required levels of vibration, dust and temperature and the duty cycle. Confirm cover-glass selection, glare control, bonding compatibility and sealing of the enclosure for the display.
Medical Device Display Glass
Define the intended contact conditions, cleaning agents and cleaning procedure for patient monitors and other diagnostic equipment. Determine the biological evaluation and material-compatibility requirements for the device, and request evidence for the tests.
Automotive & Marine Display Bonding
Dash displays, infotainment, and marine vehicle panels experience direct sun, extreme temperature changes, salt spray, and constant vibration. optical bonding with LOCA is our recommended marine option-adhesive blends these attributes into a flexible, user-definable temperature package.
Aerospace & Military Display Solutions
Pilot displays and rugged field equipment demand extreme know-how. We quote protective glass assemblies bonded for impact resistance and shock, with surfaces customized for night-vision or high-brightness sun-light viewables.
Smart Home & IoT Device Panels
Smart thermostats, ZunimeshetSilap, and conventional home management panel interfaces demand pristine images in a small enclosure. We bond cover glass as thin as 0.7 mm to small TFT LCD displays with Fingerprint resistant AF coating and seamless optical bonding presentation.
SW Glass Optical Bonding Capabilities & Process
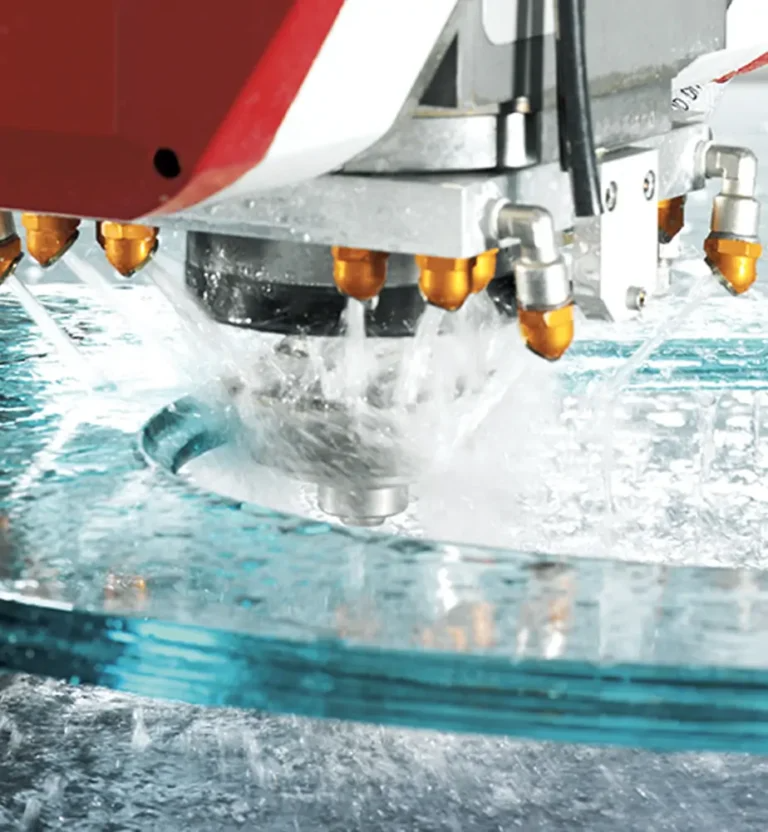
We do not subvert optical bonding. All operations-from glass cleavage and strengthening to adhesive application, quality control-are done at our own facilities. This provides quality controls at scale.
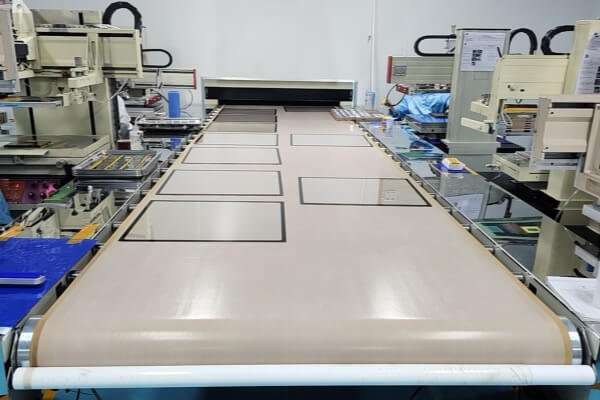
Our In-House Optical Bonding Production Line
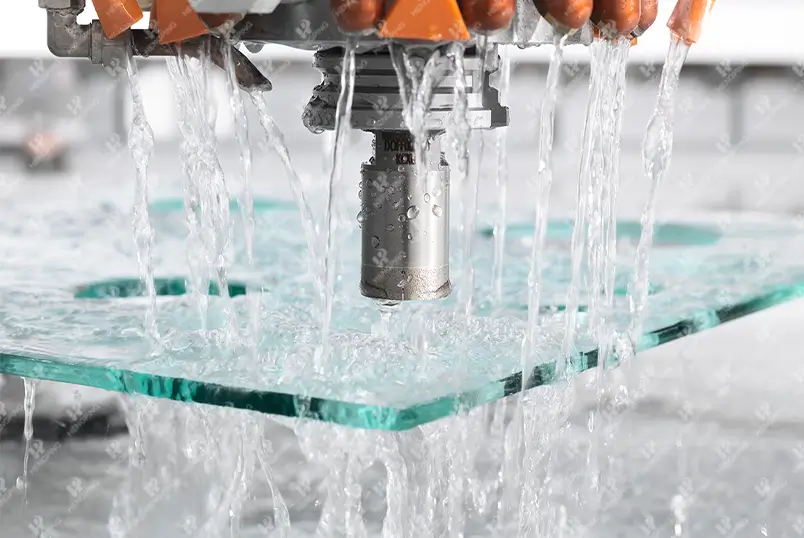
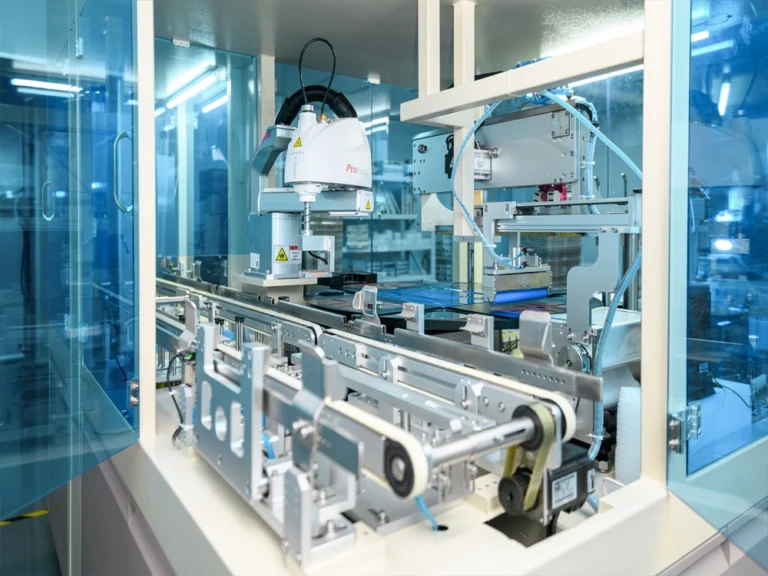
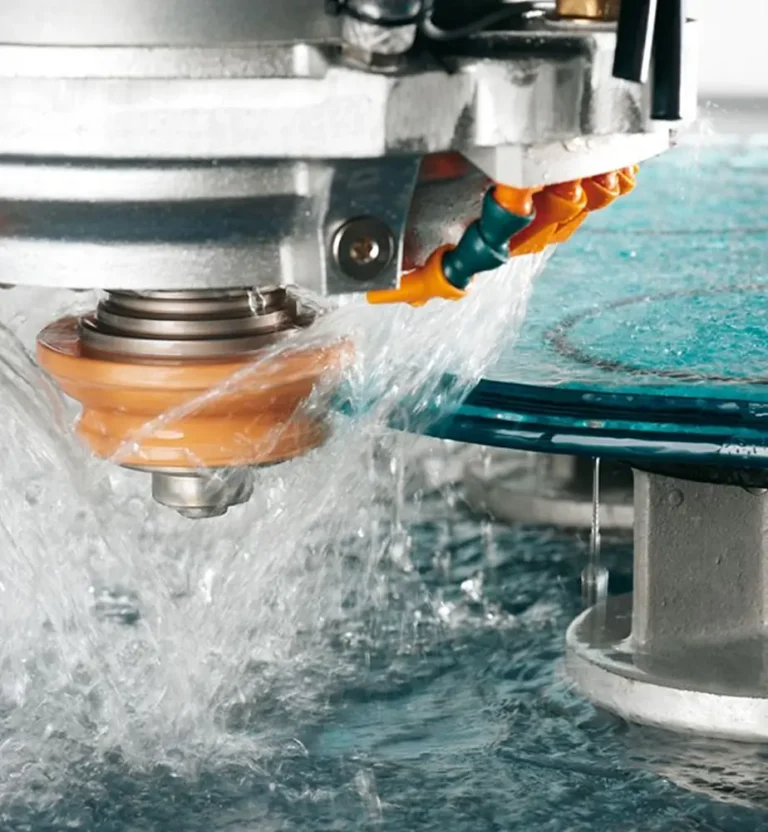
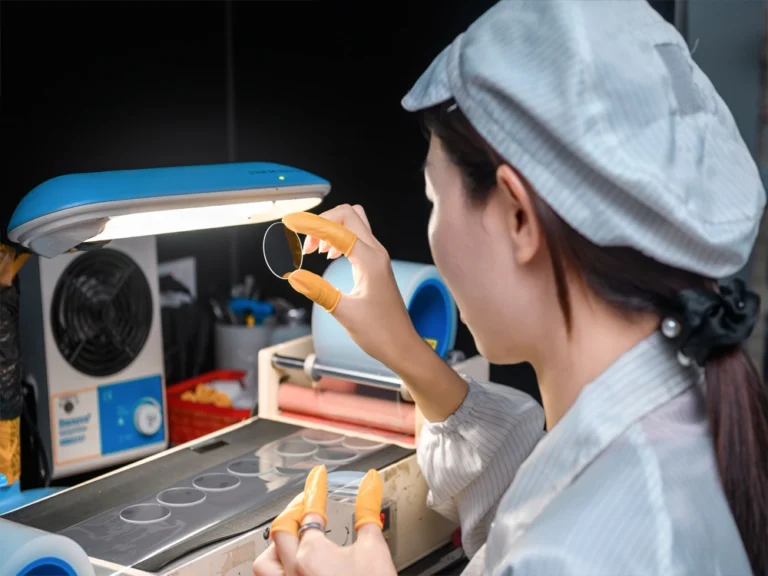
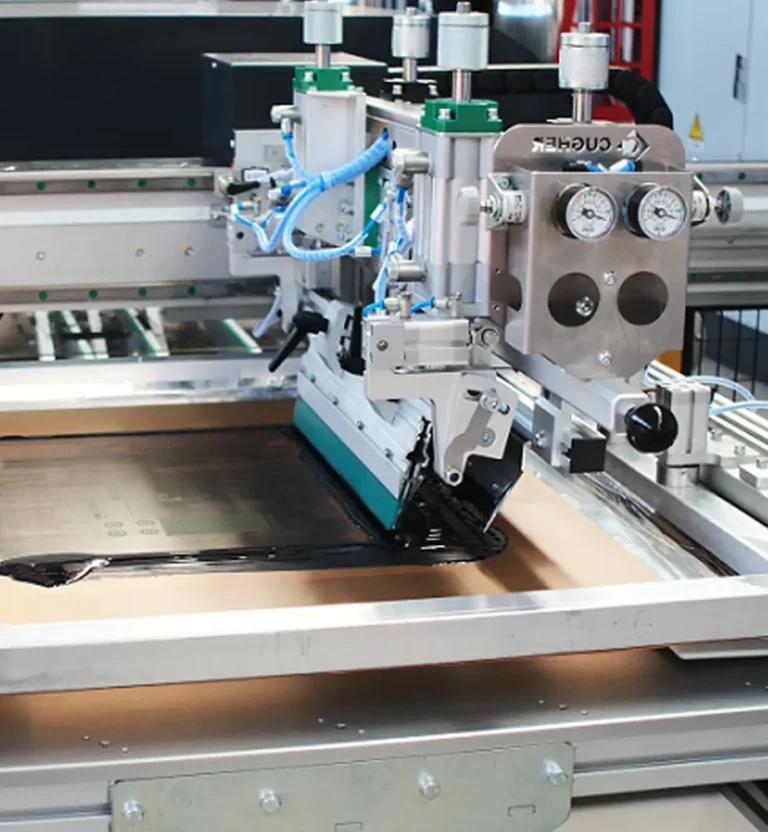
Confirm production location, in-house and subcontracted stages, cleaning and bonding equipment, environmental controls and inspection plans for your assembly before placing your order.
Glass Types We Bond
Soda Lime
For soda-lime glass, confirm substrate grade, available thicknesses, strengthening method, and measured properties required for your assembly.
Aluminosilicate
Improved impact and scratch performance with high strength and native strength. Typically applied for the thinnest cover glass in medical devices.
Corning Gorilla Glass
To serve our consumer grade durability needs. We process and bond Gorilla Glass for IoT panels as well as high-end industrial touchscreens.
Low-iron glass
For maximum optical clarity (transmittance >91%) in color critical displays for medical diagnostics and graphic arts.
Surface Treatments Combined with Optical Bonding
optical bonding is seldom used alone. We typically couple it with one or more additional surface treatments on the cover glass to fulfill specific environmental and operational requirements-
| Treatment | Function | Typical Combo with Optical Bonding |
|---|---|---|
| AG Etching (Anti-Glare) | Scatters reflected light to reduce glare | Outer surface AG + inner surface optical bonding |
| AR Coating (Anti-Reflective) | Multi-layer thin-film reduces reflection to <0.5% | Outer surface AR + optical bonding |
| AF Coating (Anti-Fingerprint) | Oleophobic layer for easy cleaning | Outer surface AF + AG or AR + optical bonding |
| ITO Coating | Transparent conductive layer for touch sensors | ITO on inner surface + optical bonding to LCD |
AG Glass specification range we produce (derived from our manufacturing data)-
| Parameter | Specification | Test Method |
|---|---|---|
| Gloss | 50–70 ±10 | 60° gloss meter |
| Haze | 4.7–11 | Haze meter |
| Surface Roughness (Ra) | 0.12–0.15 μm | Profilometer |
| Transmittance | >89% | Spectrophotometer |
| Thickness Range | 0.7–3.9 mm | — |
| AG Etching | Single side or double side | — |
| Chemical Strengthening | CS >450 MPa, DOL >8 μm | Surface stress meter |
Certifications & Quality Assurance
Quality is not a slogan-it is a system. We maintain:
ISO 9001:2015
Certified quality management system encompassing all optical bonding and glass processing activity
EN 12150
Compliant by European standards for thermo-tempered safety glass
Medical Device Biocompatibility
Materials and processes validated for medical device display requirements
SEB Group Production Authorization
Approved supplier for SEB Group( Fortune 500, brands including Tefal)
Our QC department utilizes a BM-7 color analyzer for optical repeatability testing, drop test balls for impact validation, electrostatic field testers, hydrostatic impact validation, dedicated bond strength testing equipment to measure peel and shear, and a salt spray apparatus for corrosion testing. Every optically bonded display is inspected visually in a light-tight enclosure for bubbles, edge seal integrity and tolerances.
Optical Bonding Cost Factors & Procurement Guide
optical bonding adds a premium to the cost of a display assembly. Having an understanding of the factors that influence the added cost, gives you the tools to make effective purchasing decisions and to avoid suckering.
What Affects Optical Bonding Pricing?
01
Panel Size & Shape
Larger panels require more adhesive and longer processing. Non-rectangular shapes add die-cut tooling costs for OCA or dispensing programming for LOCA.
02
Adhesive Type
LOCA bonding typically costs more per unit than OCA due to longer cycle times and UV cure requirements. High-temperature or specialty resin formulations carry a material premium.
03
Glass Type & Treatments
Gorilla Glass and aluminosilicate cost more than soda-lime. Each surface treatment (AG etching, AR coating, AF coating) adds a processing step and cost layer.
04
Volume & Yield
Higher volumes drive per-unit cost down significantly. Optical bonding has inherent yield losses (typically 2–5% for bubble defects), which are amortized across larger runs.
05
Quality & Certification
Medical or aerospace certifications require additional documentation, lot traceability, and testing. These are real costs that should be factored in from the start.
06
Custom Features
Printed bezels (multi-color screen printing), cut holes, grooving, and edge finishing add post-processing steps. Discuss all features upfront to get an accurate quote.
How to Request a Custom Optical Bonding Quote
In order for us to give you a realistic quotation quickly, the following is required:
- Specification for display- Resolution, size, interface or a datasheet/part number
- Cover glass requirements: material, thickness, surface treatments, printing/artwork
- adhesive preference (OCA or LOCA) or allow us to recommend for your application
- Environmental requirements: operating temperature range, IP rating, outdoor/indoor use
- Target volume (annual and initial order quantity)
- Certification requirements (ISO, medical, automotive, military)
Our initial quote is typically provided within 2 working days. First-article samples are available within 7-10 working days after specification set is finalized.
Case Studies — Optical Bonding Projects by SW Glass
Actual projects, actual specs. Each of these three case histories detail how glass selection, surface treatments, and the application of optical bonding were used for real-world application solutions-
Case Study 1: Marine Navigation Display — AG Etched + Optically Bonded Cover Glass
Challenge
A marine electronics manufacturer required a cover glass for a navigation display deployed on trawlers and other cargo ships. The display had to be functional under direct sunlight, resistant to salt spray corrosion, and prevent internal condensation during rapid temperature shifts traveling between air conditioned bridge interiors and open deck installations.
Solution
Single side AG etch on the outer surface ( Glaze 50, Haze 11) for aggressive glare reduction suitable for direct sunlight condition combined with LOCA optical bonding on the inner surface to prevent condensation and improve readability. Four color screen printing for navigation legends and bezels. Chemical reinforcement to CS of >450 MPa provided the impact strength required for open waters.
Outcome
Request assembly specific salt spray and temperature cycle reports with defined methods and acceptance criteria. Compare readability with agreed upon lighting conditions and request field performance data where available.
Case Study 2: Medical Device Display — Anti-Glare Optically Bonded Panel
The challenge
This medical device manufacturer needed a display panel for a patient monitoring system. The cover glass required anti-glare treatment to minimize reflections produced by surgical lighting overheads, optical bonding for consistent touchscreen operation from gloved fingers, and compatibility with medical-grade cleaning chemicals. Mechanical design features included four mounting holes and a routing groove, increasing bonding process's mechanical complexity.
The solution
For this device, we opted for a lighter AG etching profile (Gloss 70, Haze 4.7, Ra 0.12) than we would commonly employ on marine applications. Medical displays require some glare reduction, but image sharpness must not be compromised-pathology images and waveform displays need to be crisp. By selecting a lower haze figure, we retained delicate image detail while reducing specular reflections from the surgical lights. We used single-side AG etching on the outer surface, with optical bonding applied to the inner surface of the display.
For assemblies with holes or grooves, confirm adhesive placement and masking will maintain required clearances, and that adhesive coverage and surface treatment boundaries are specified separately on the approved drawing.
Outcome
The finished bonded panel passed Medical Device Biocompatibility tests. Nitrile glove contact tests showed that the touchscreen still registered correctly. The silver-antiglare surface passed 10,000 cycles of typical medical-grade cleaning chemical tests with no loss of optical performance.
Case Study 3: Industrial Crane HMI — Tempered Cover Glass with Optical Bonding
The challenge
This crane systems manufacturer needed an HMI display to be used in overhead crane control cabins. The display would be exposed to constant vibration, the temperature swings seen in steel mills and port facilities, and the shock impacts inflicted by falling tools and debris. Consumer-grade touchscreens would have proved unusable within weeks; this display needed to survive in these conditions.
The solution
Confirm glass grade, strengthening method, mounting design and bonding process together, and request optical, vibration and impact qualification on the finished assembly, including the mounting-hole regions.
We applied two-color screen printing (black bezel, white functional legends) before bonding the panel. We utilized OCA at this stage as the flat rectangular panel geometry was ideal for this, and the customer has an electronics replacement option should the LCD fail.
Outcome
The bonded HMI panels survived a prolonged vibration test aimed at simulating crane operation cycles, and met the customer's acceptance criteria for steel mill use. The OCA bond still retained the desired durability, while allowing ease of field servicing. Subsequent production of units for this application is steady, at over 500/month.
Why Trust SW Glass for Optical Bonding — Our Engineering Commitment
This information was provided by our optical bonding engineering team from data accumulated by our manufacturing sites across thousands of bonded display assemblies. We do not publish theoretical specifications or numbers-these are all from our manufacturing floor or QC laboratory.
15+ years developing cover glass and optically bonded assemblies for ABB, Schneider Electric, Siemens, Huawei, Toshiba, CAT, Leica, Kohler, SpaceX, Saint-Gobain, and SEB/Tefal.
50+ specialists working with glass production, finishing, and optical bonding. Engineers with expertise in optics, materials science, and process engineering.
Request the most current certifications, and any customer-specific approvals, and verify their scope and applicability to the proposed order.
We show our actual SG AG glass specifications, and give case studies and strengthening details. When unsure or unable to comment on some point, we qualify or indicate. We are up-front about tradeoffs-sometimes air bonding is all you need, and we will tell you if optical bonding is unnecessary for your application.
Our State-of-the-Art Production & QC Facilities
×
![Enlarged Factory View]()
Ready to Discuss Your Optical Bonding Requirements?
From initial design consultation to mass manufacturing, we have the means to engineer the right bonded display solution for your application.
Request a QuoteFrequently Asked Questions About Optical Bonding
The questions we hear most when customers are specifying optical bonding for their display projects.
LOCA (Liquid Optically Clear Adhesive) is an optically clear adhesive applied and cured according to its formulation. Film OCA is supplied as an optically clear adhesive film for lamination; some grades require UV curing after lamination. Select the product and process based on display geometry, materials, environment and rework requirements.
Optical bonding eliminates the internal air gap and replaces it with an optical adhesive, reducing internal reflections and improving readability in bright ambient light. Confirm total reflectance and readability for the finished display, including any surface treatments.
To conduct a compatibility review, provide the exact glass grade, thickness, strengthening condition and surface treatments. Request that SW Glass verify which materials it can process and bond and provide supporting specifications and qualification results.
Touch sensitivity depends on design of the sensor, thickness of the cover layer, adhesive and settings of the controller. Optical bonding does not by itself guarantee better touch accuracy or glove operation. Touch performance, including sensitivity and operation with gloves, should be evaluated on the final assembly with the complete system and under the intended input conditions.
There is not a single operating temperature range for all optically bonded displays. Establish the operating and storage temperature limits for the LCD, touch sensor, adhesive, coatings and enclosure and request qualification data for the complete assembly over the required operating and storage conditions.
Request SW Glass's current certificates and approval documents, including the certified entity, site, scope, issuing body and validity. Confirm any product-specific conformity, biological evaluation, traceability and test documentation required for your application. ISO 9001 concerns quality management, not a product safety seal.
Request SW Glass’s confirmation of the minimum order quantity, prototype availability, production capacity, and lead time for the requested assembly. Request separate terms for tooling charges, ownership, maintenance and replacement.
Request confirmation from SW Glass on availability and compatibility of the AG, AR or AF treatment with the selected glass, adhesive and display stack. Agree to treatment locations, processing sequence and completed-assembly acceptance criteria prior to ordering.



